

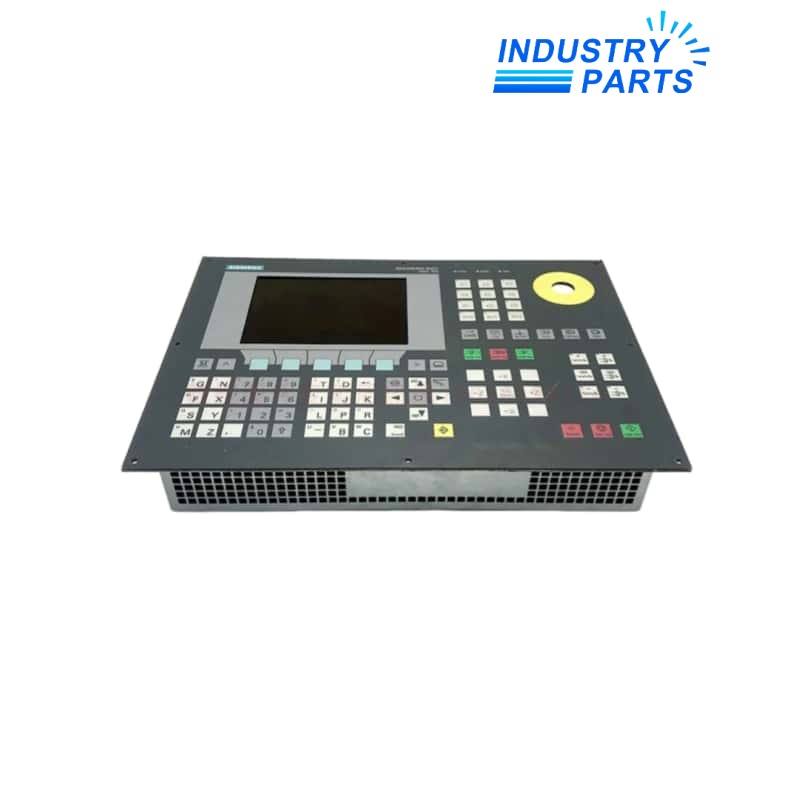
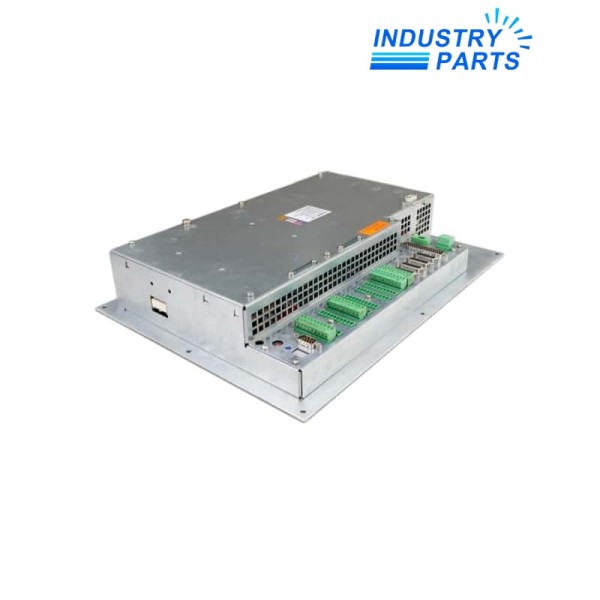
Siemens 6FC5500-0AA11-1AA0 SINUMERIK 802C Base Line Basic Package
01Product Overview
Siemens 6FC5500-0AA11-1AA0 is the SINUMERIK 802C Base Line basic package for compact machine-tool control. The official package includes the operator panel control, machine control panel, peripherals, 48 digital inputs, 16 digital outputs, toolbox and logbook. Commissioning depends on the exact turning or milling application, encoder setup, PLC program, machine data and saved production archive.
02Performance
Operating Capabilities
- Combines the core 802C Base Line operator and machine-control components in one documented package.
- Provides 48 digital inputs and 16 digital outputs for the basic machine I/O architecture.
- Supports systematic startup of encoders, PLC, axes, spindle and general machine data.
- Supports transfer and service tasks through the documented Toolbox and WINPCIN workflow.
- Allows the documented turning or milling cycle package to be handled within the applicable configuration.
- Requires final axis, spindle and drive optimization before production release.
Product Identity
- Manufacturer: Siemens
- Model: 6FC5500-0AA11-1AA0
- Product Type: SINUMERIK 802C Base Line basic control package
- Status: Officially identified as spare part
03Technical Details
| Manufacturer | Siemens |
|---|---|
| Article Number | 6FC5500-0AA11-1AA0 |
| Product Designation | SINUMERIK 802C Base Line Basic Package |
| Package Component | Operator panel control |
| Machine Interface | Machine control panel and peripherals |
| Digital Inputs | 48 |
| Digital Outputs | 16 |
| Service Resources | Toolbox and logbook |
| Transfer Utility | WINPCIN for documented V24 data transfer |
| Application Packages | Documented turning or milling cycle package |
| Commercial Position | Spare part |
04System Integration
- Identify whether the installed machine uses the turning or milling configuration before restoring cycles.
- Back up PLC, machine data, tool data, zero offsets and production settings.
- Verify encoder assignment, axis direction, measuring system, spindle feedback and limit configuration.
- Check the 48/16 digital I/O mapping against the machine wiring and PLC program.
- Use the documented V24 and WINPCIN transfer procedure when applicable to the installed system.
- Complete startup in the official sequence and save a validated final archive.
05Applications
- Compact turning machines using the SINUMERIK 802C Base Line architecture.
- Compact milling machines configured for the supported 802C cycle environment.
- Spare-part restoration of installed operator-panel and machine-control packages.
- Machine rebuilding where the original encoder, I/O and PLC documentation is available.
- Maintenance projects requiring controlled V24 transfer and archive restoration.
- Legacy machine-tool service where axes, spindle and drives can be recommissioned completely.
06FAQ
Which hardware is included in the 6FC5500-0AA11-1AA0 basic package?
The official package identifies the operator panel control, machine control panel, peripherals and 48/16 digital I/O, together with the toolbox and logbook.
How should a turning configuration be distinguished from a milling configuration?
Confirm the installed cycle package, PLC project and machine data before loading; the two application configurations must not be interchanged casually.
What is WINPCIN used for on this SINUMERIK package?
The Siemens startup documentation uses WINPCIN for applicable V24 data transfer and service operations.
Which commissioning stage comes before drive optimization?
Encoder, PLC, general machine data, axis-specific data, spindle matching and basic axis or spindle tests must be established before final optimization.
Why must the 48-input and 16-output map be preserved?
The physical machine wiring and PLC logic depend on the original digital-I/O assignment, so an incorrect map can cause missing or unsafe machine behavior.
What should the final 802C acceptance test cover?
Confirm axis direction and referencing, spindle feedback, limits, PLC interlocks, all I/O, alarms, cycles and the complete turning or milling process before saving the final archive.
+Recommended Models
| P78LCA-9300 | ABB YO-1SDA038291R1 YC-1SDA038301R1 | 140DDI35300 |
| 1-Q-EC 230572 | NTPS-24-1.3 | MCR-F-UI-DC 2814605 |
| P8 R8 DIN - 8 | GE 3000 | Z954 071863 |
| IHRT46B/4D | C7973A LTO-3 | EKA173/5 |
| Siemens 3TF3001-0XL2 | ABB 1SDAO13856R1 | EC3-X32 |
| RMT2#A5LL000 | FGR55-8-10 | 506001MED-8017X |
| CMDSLCZBU | FMC250 | C-Bus2 L5504RVF L5504RVFP |
| SEC-TEA-230-5045 | EX1N32ER | GCD-0001 8XP-W |
| D5290S-078 | FS-B3510 | 3HE05833CAAA01 |
| ABB MU6301/60-811-500 | N500W | 1768-ENBT/A PN-14845 |


